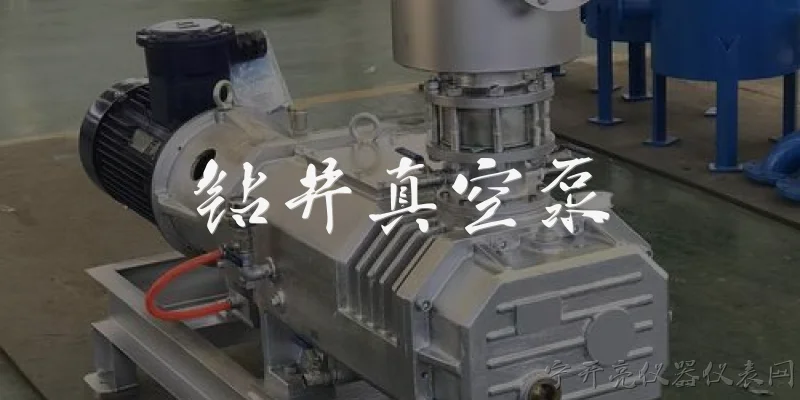
Drilling vacuum pump:What is a drilling vacuum pump and what is its primary function?
Q: What is a drilling vacuum pump and what is its primary function?
A: A drilling vacuum pump is a specialized piece of equipment used in drilling operations to manage gases and fluids encountered downhole. Its primary function is to create a vacuum that removes air, gas, or liquid from the borehole or drilling system, preventing kicks, blowouts, and maintaining wellbore stability. In drilling rigs, these pumps are often part of a vacuum degasser system, which separates entrained gases from drilling mud. By reducing pressure in the annulus or suction line, they help control formation pressures, improve drilling efficiency, and ensure safety by mitigating hazardous gas accumulation.
Q: How does a vacuum pump contribute to well control during drilling?
A: During drilling, a vacuum pump enhances well control by removing formation gas from the drilling fluid before it returns to the surface. When gas enters the mud, it reduces hydrostatic pressure and can lead to kicks. A vacuum pump, typically in a vacuum degasser, applies negative pressure to the mud, causing dissolved and entrained gases to break out and be vented safely. This restores mud density, maintains the required hydrostatic head, and prevents gas from reaching the rig floor. Additionally, it helps monitor gas levels, allowing early detection of kicks and enabling timely shut-in procedures. Thus, it is a critical safety component in managed pressure drilling.
Q: What are the common types of vacuum pumps used in drilling operations?
A: In drilling operations, the most common vacuum pumps are liquid ring vacuum pumps and rotary vane vacuum pumps. Liquid ring pumps are preferred for vacuum degassers because they handle wet, dirty gases and liquids well, using water or oil as the sealing liquid. Rotary vane pumps are used in smaller applications, such as vacuum-assisted mud logging or sample collection, due to their compact size and high efficiency at lower flow rates. Other types include dry screw pumps for oil-free environments and ejector-based vacuum systems for hazardous areas. Selection depends on mud properties, gas load, and explosion-proof requirements.
Q: What maintenance practices are essential for drilling vacuum pumps?
A: Essential maintenance for drilling vacuum pumps includes regular inspection of seals, bearings, and impellers for wear, and checking the sealing liquid quality and level in liquid ring pumps. The vacuum pump oil in rotary vane types must be changed per manufacturer intervals to avoid contamination. Filters and strainers should be cleaned to prevent debris from entering the pump. Monitoring vacuum level and motor current helps detect performance issues early. In drilling environments, explosion-proof motors and electrical components require periodic checks. Also, after each well section, flush the pump with clean water or solvent to remove mud and gas residues, preventing corrosion and clogging.
Q: What safety considerations apply when using vacuum pumps in drilling?
A: Safety considerations for drilling vacuum pumps include ensuring all electrical components are explosion-proof and properly grounded to prevent ignition of flammable gases. Vacuum pump exhaust must be routed to a safe, well-ventilated area away from ignition sources and personnel. Regular gas monitoring around the pump is critical, as it may release toxic or combustible vapors. Operators should wear appropriate PPE, including gas detectors and fire-resistant clothing. Pressure relief valves and flame arrestors should be installed to prevent overpressure and flashback. Training on emergency shutdown procedures and proper handling of sealing liquids, which may contain hazardous contaminants, is also essential.
Dialogue about
Common scenarios of "Drilling vacuum pump"
【Drilling Engineer】 Hey, I'm having trouble with the vacuum pump on the drilling rig. It's not maintaining the required vacuum level.
【Vacuum Pump Technician】 I see. Let's troubleshoot. What's the current vacuum reading?
【Drilling Engineer】 It's fluctuating around -0.6 bar, but we need it at -0.8 bar for proper degassing.
【Vacuum Pump Technician】 Have you checked for leaks in the suction line?
【Drilling Engineer】 Yes, we did a soap bubble test and found no leaks.
【Vacuum Pump Technician】 How about the inlet filter? Is it clogged?
【Drilling Engineer】 We replaced it last week, so it should be fine.
【Vacuum Pump Technician】 What about the vacuum pump oil? When was it last changed?
【Drilling Engineer】 Oil was changed about 500 hours ago. The level is okay, but it looks a bit dark.
【Vacuum Pump Technician】 That could be an issue. Contaminated oil can reduce pump efficiency. I recommend changing it.
【Drilling Engineer】 Okay, we'll change the oil. But could there be other causes?
【Vacuum Pump Technician】 Possibly. Check the exhaust filter and the separator element. If they're clogged, it can cause back pressure.
【Drilling Engineer】 We'll inspect those. Also, the pump seems to run hotter than usual.
【Vacuum Pump Technician】 Overheating can be due to poor ventilation or internal wear. Are the cooling fins clean?
【Drilling Engineer】 They have some dust buildup. We'll clean them.
【Vacuum Pump Technician】 Good. Also, check the drive belt tension. A loose belt can reduce pump speed.
【Drilling Engineer】 We'll check that. What about the vacuum relief valve?
【Vacuum Pump Technician】 Yes, if it's stuck open, it won't hold vacuum. Test it manually.
【Drilling Engineer】 Okay, we'll do that. If none of these fix it, what then?
【Vacuum Pump Technician】 Then it might be internal wear like vanes or bearings. You'll need to schedule a rebuild.